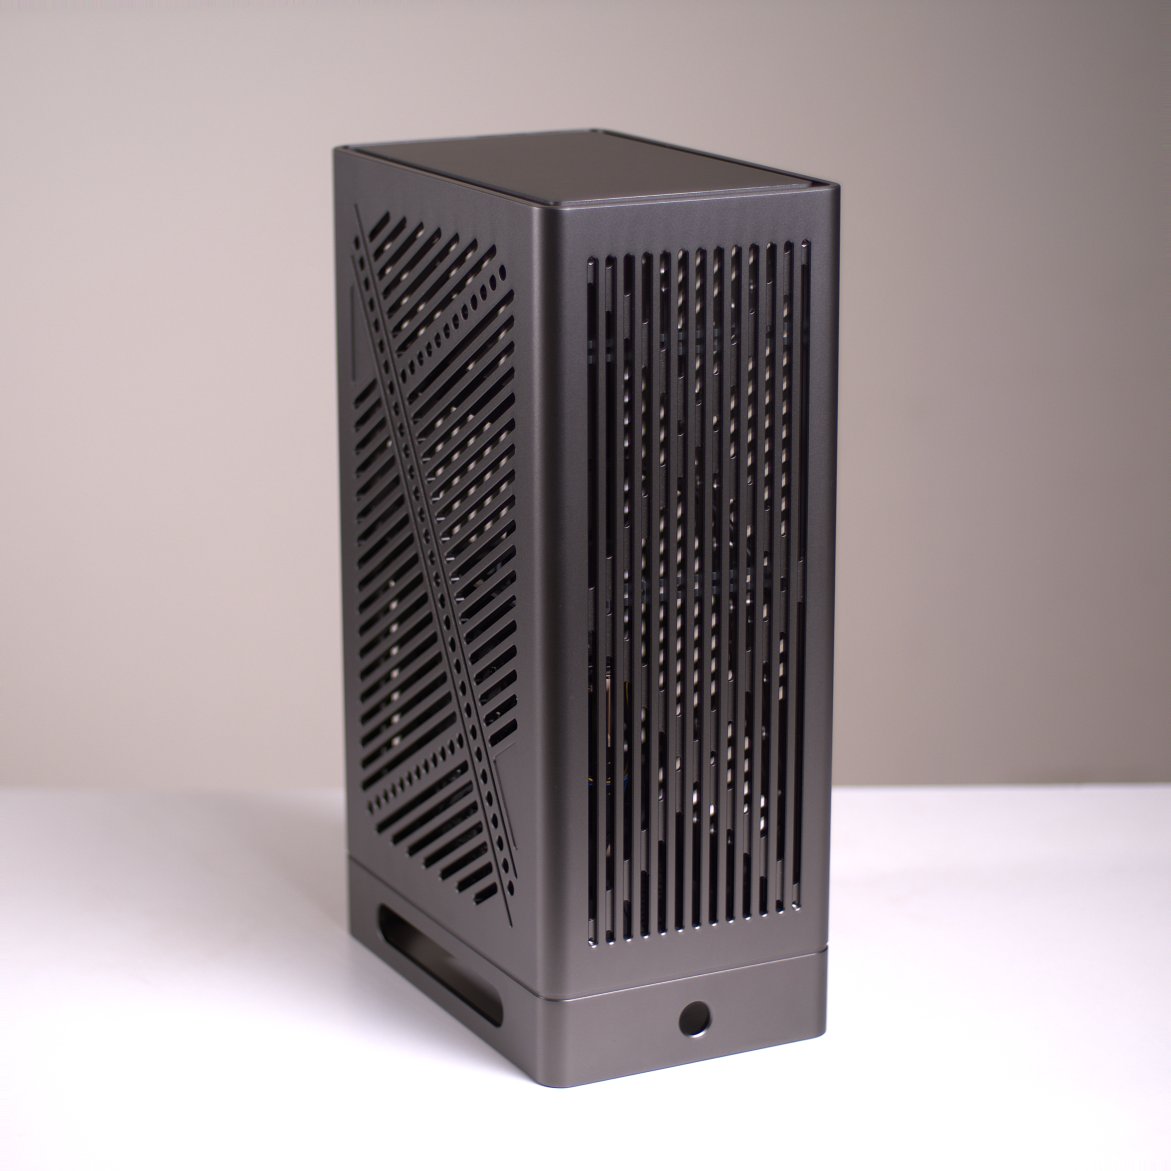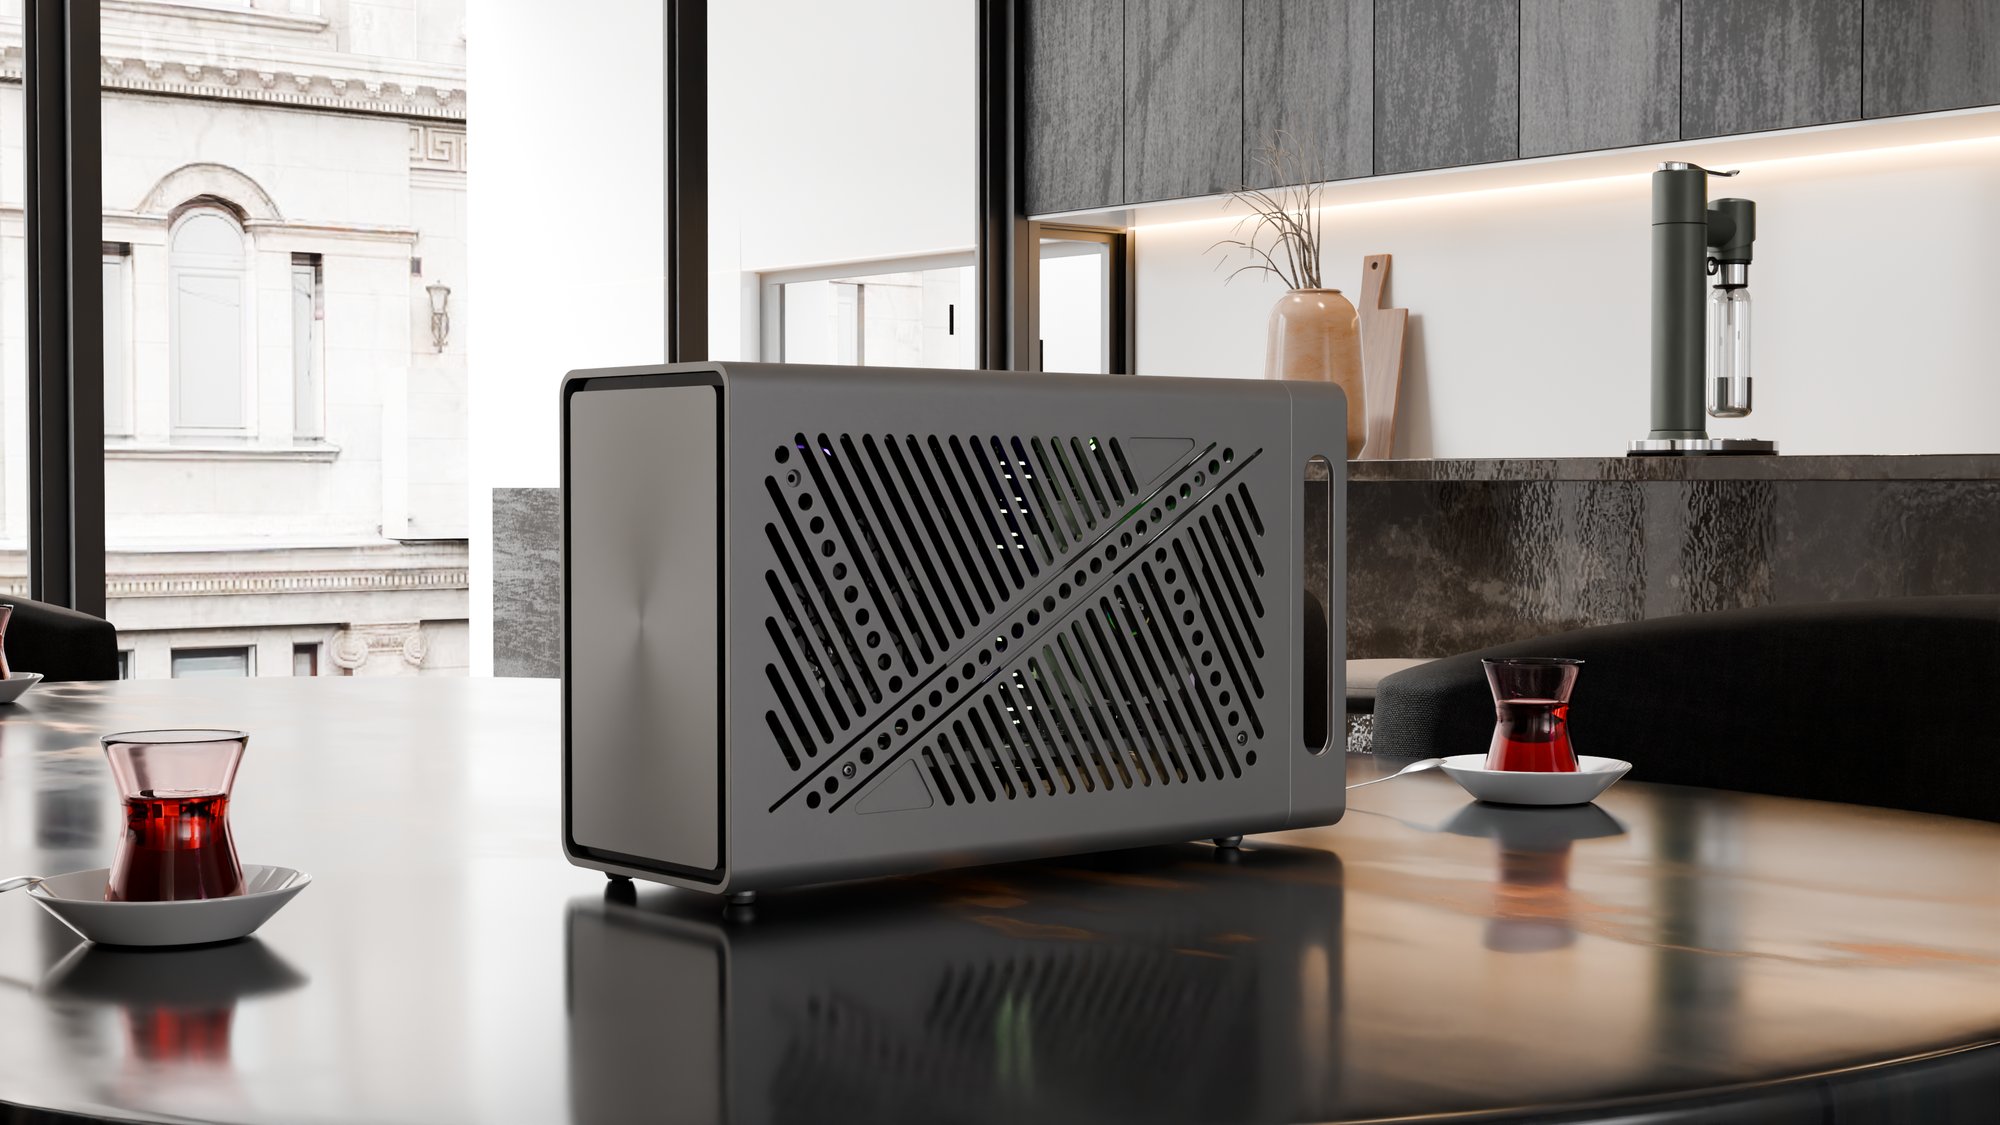
This isn't a sheet-metal shell. It's a hollow profile extruded from a heated aluminum billet under high pressure. The larger, thicker, and more complex the cross-section, the harder it is to control die flow, temperature, and puller straightening — otherwise straightness, seam position, and surface quality become unstable.
Extrusion defines the overall structure; CNC defines the details and precision. Ports, mating faces, ventilation cutouts, chamfers, and more are milled under coolant to achieve strength, finish quality, and tight assembly consistency. Final step: precision CNC machining + fine-bead sandblasted anodizing.